I. Key Purchasing Criteria and Technical Evaluation Dimensions
1. Carrier Resin Compatibility
Homogeneous/Specialized Carrier (Highly Recommended): High-quality PET masterbatches must utilize premium virgin low-viscosity or modified PET polyester as the carrier. This ensures 100% compatibility with the base resin without compromising the mechanical strength or optical properties of the finished product.
Intrinsic Viscosity (IV) Matching:
The carrier's IV value must be selected based on the end-use application. Typically, a low IV (e.g., 0.55–0.65 dL/g) is chosen to facilitate better pigment wetting and dispersion; however, the IV must not be excessively low, as this would dilute the viscosity of the base resin.
Prohibited Materials: The use of low-melting-point, low-molecular-weight waxes (such as PE wax or EVA carriers) is strictly prohibited in injection molding, blow molding, film stretching, and fiber spinning. EVA undergoes thermal decomposition at temperatures exceeding 230°C, releasing acetic acid; this not only severely degrades PET melt strength-causing yellowing and brittleness-but also corrodes screws and molds.
2. Temperature Resistance and Heat Stability
The melt processing range for PET is typically 260°C–290°C, reaching up to 300°C for specific high-temperature spinning or thick-walled injection molding processes, with melt residence times usually ranging from 3 to 10 minutes.
Colorant Temperature Resistance Rating: Selected organic pigments, solvent dyes, or inorganic pigments must withstand temperatures of ≥ 280°C–300°C (per DIN EN 12877 standards) and exhibit no significant color deviation (ΔE < 1.0) within the processing residence time.
Sublimation Resistance: During high-temperature vacuum degassing or drying stages, low-molecular-weight colorants are prone to volatilization and sublimation, which can contaminate mold vents, rollers, or drying tower filters. Consequently, the molecular weight and sublimation resistance rating of the colorants must be rigorously evaluated. 3. Moisture Control and Drying Compatibility
Hydrolysis Sensitivity: In the molten state, even trace amounts of moisture rapidly trigger polyester chain scission via hydrolysis. This manifests as a drastic drop in Intrinsic Viscosity (IV), the appearance of "silver streaks" or bubbles in the finished product, and embrittlement or cracking.
Factory Moisture Specifications: For high-quality PET masterbatches, factory moisture content must be strictly controlled at ≤ 0.05% (500 ppm); for high-end ultra-thin film or fiber-spinning grades, it should be ≤ 0.03% (300 ppm).
Drying Hopper Compatibility: Most PET production processes require dehumidifying drying at 140°C–160°C for 4–6 hours. If the masterbatch has not undergone sufficient crystallization (i.e., it remains amorphous), it will soften, stick together, and form clumps ("bridging") when the temperature in the drying hopper exceeds the glass transition temperature (Tg ≈ 78°C). When sourcing, it is essential to verify whether the masterbatch is pre-crystallized and capable of withstanding these drying conditions.
4. Dispersion and Filter Pressure Value (FPV)
Agglomerate Control: Colorant primary particle sizes are typically in the micron range. If dispersion within the masterbatch is inadequate, secondary agglomerates can lead to bottle preform breakage during blow molding, "fish eyes" (gels) in films, and filament breakage in synthetic fibers.
Filter Pressure Value (FPV) Testing:
Synthetic Fiber Spinning Grade (POY/FDY): Strict requirements; FPV typically needs to be ≤ 1.0–1.5 bar/g (tested using a 1400-mesh screen), with a particle size of ≤ 2 μm.
BOPET Film Grade: FPV should be ≤ 1.5–2.0 bar/g. Injection Molding & Preform Grade: No macroscopically visible impurities or color specks on the surface; FPV ≤ 3.0 bar/g.
5. Migration Resistance & Weatherability
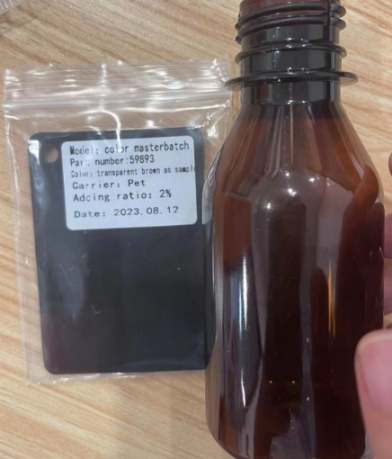
Solvent/Oil Migration Resistance: When using solvent dyes for transparency, the compatibility and fixation of the dye within the polyester polymer chains must be verified to prevent migration into contents such as oily substances, alcohols, or carbonated beverages.
Lightfastness/Weatherability Grade:
Indoor household goods/packaging: Lightfastness ≥ Grade 6 on the Blue Wool Scale.
Outdoor PET fabrics, sheets, and shading structures: Lightfastness Grade 7–8; Weatherability Grey Scale ≥ Grade 4.
6. Impact on Crystallization (Nucleation Effect)
Certain inorganic pigments and phthalocyanine pigments (e.g., Phthalocyanine Blue, Phthalocyanine Green) exhibit strong heterogeneous nucleation effects, significantly raising the PET crystallization temperature (Tc) and accelerating the crystallization rate.
Potential Consequences: Localized spherulite growth during the molding of transparent preforms or sheets, resulting in "whitening" or haziness; anisotropic shrinkage in injection-molded parts, leading to warpage and deformation.
Countermeasures: For transparent parts, select polyester-specific dyes or sparingly soluble polyester pigments with low or no nucleating activity; for structural injection-molded parts, use surface-modified masterbatches designed for low shrinkage and warp resistance.